 Skip to content
Specialized Facility Floor Coatings in The Rochester, MN Area
- One Day Installations Available
- fully Free Honest Estimates
- Honest Work Backed by Real Results
Get a Free Quote Today
Facility Floor Coatings: The floor is an integral part of your operation, no matter if you’re in food processing, manufacturing, aviation, or any industry. It has to resist harsh chemicals, withstand heavy machinery, and meet strict regulatory standards. A failing floor isn’t an inconvenience; it’s a failure that can lead to downtime, contamination, and safety incidents.
At Midwest Surface Coatings, we develop specialized facility floor coatings in Rochester for the most demanding environments. We don’t believe in one-size-fits-all solutions. We understand your specific processes, challenges, and compliance needs to install a flooring that contributes to the safety, efficiency, and success of your operation. Ready to discuss a flooring system engineered for you?
Wrong Floor is a Liability, Right Floor is an Asset
Facility Floor Coatings: This is our saying about floors at Midwest Surface Coatings. Standard concrete or an improperly specified coating system will fail in a true industrial setting. Our systems solve the most critical problems facilities face.
- Attack & Erosion
The harsh acids, alkalis, and solvents used in many industries will eat away at bare concrete and destroy lesser coatings. We install truly chemical-resistant floor coatings in MN to withstand your exact chemical profile.
- Sanitation Issues
Cracks, pores, and seams in a floor are breeding grounds for bacteria. It makes sanitation difficult. Our flooring for factories provides a smooth, non-porous surface that meets USDA and other standards.
- Impact Damage
Heavy equipment, dropped tools, and traffic can chip, gouge, and wear down unprotected concrete. Our high-build systems handle extreme impact and abrasion resistance.
- Safety Hazards
Spills, moisture, and poor lighting create constant safety risks. We make our floors with slip-resistant textures, and we add bright safety line striping to protect your team.

An Engineered Industrial Facility Floor
A correctly specified flooring system is a powerful investment in your facility’s future.
- Chemical Resistance
Protect your concrete slab from corrosion and your business from hazardous spills with a floor that is impervious to your specific chemicals.
- Enhanced Safety Compliance
A slip-resistant and properly marked floor reduces workplace accidents and exceeds industry regulations.
- Extreme Durability
Our floors withstand the daily abuse of heavy machinery, thermal shock from steam cleaning, and constant wear, drastically reducing repair costs and downtime.
- Superior Sanitation
A non-porous floor is incredibly easy to clean and sanitize, and saves labor costs.
The Right System for Your Operations
Facility Floor Coatings: We offer high-performance floorsand will help you select the precise one for your facility’s needs.

01Urethane Cement Systems
The gold standard for the food and beverage industry. Urethane cement offers unmatched resistance to thermal shock, moisture, and organic acids.
02Novolac Epoxy Coatings
For the ultimate in chemical resistance. Novolac epoxy handles exposure to harsh acids and solvents for labs, containment areas, and chemical processing plants.
03High-Build Epoxy
This is for general manufacturing, assembly plants, and workshops for excellent all-around durability.
04Facility Support Flooring
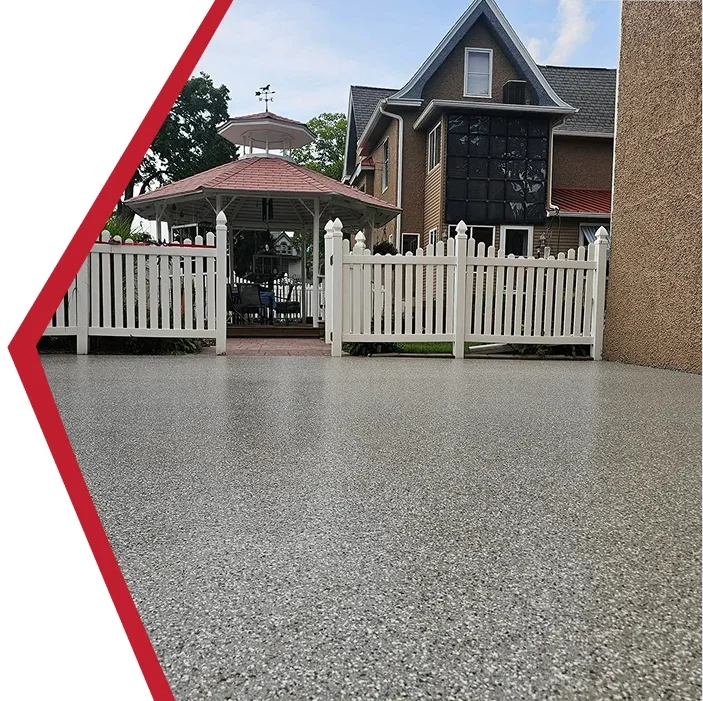
A durable and decorative Flake System Floor is perfect for locker rooms, breakrooms, and offices.
Our Facility Floor Coatings Process
A high-performance floor requires a high-precision installation.
01Facility Consultation
We analyse your operations, exposure, traffic patterns, and compliance to specify the perfect flooring.
02Surface Preparation
We prepare the concrete substrate to the specific Concrete Surface Profile for your chosen system.
03Concrete & Joint Repair
We repair all cracks, spalls, and rebuild control joints for a stable foundation to withstand industrial traffic.
04Specialized Primer
We apply a deep-penetrating primer for an unbreakable bond with the concrete and block moisture.
05Chemical-Resistant Coat
We install the main body of the urethane cement, Novolac, or high-build epoxy to the desired thickness.
06Performance Topcoat
We apply the final topcoat for your specific needs, for chemical resistance, and UV stability.

Midwest surface coatings Services
When your operation depends on the performance of your floor, you need a contractor with proven technical expertise.
Deep Technical Knowledge
We are not just Facility Floor Coating installers; we are flooring system specialists. We understand chemical compatibility, mil thickness, and the engineering behind what makes a floor succeed or fail.

Our Proven Work
We have a track record of success in Rochester. We invite you to see the quality in our Past Work gallery and see all the communities we serve on our Service Areas page.

Rochester Facility Floor Coatings FAQs
What floor do I need for sulfuric acid resistance?
We create a phased plan to minimize downtime and have them back in service within 24 hours.
How long until we can resume production?
We use fast-curing polyurea options that can have your facility back in service in as little as 24-48 hours.
Can your floors meet USDA and FDA requirements?
Yes. Our coved urethane cement flooring systems meet the strict sanitation and safety standards required for food and beverage processing facilities.
Can your floors handle steam cleaning?
Absolutely. Our urethane flooring is perfect for facilities that use hot water or steam cleaning for sanitation.
Ready to install a floor that is engineered to perform?
Proudly Serving Southern Minnesota and Western Wisconsin
 Minnesota